What Is Milled Titanium?
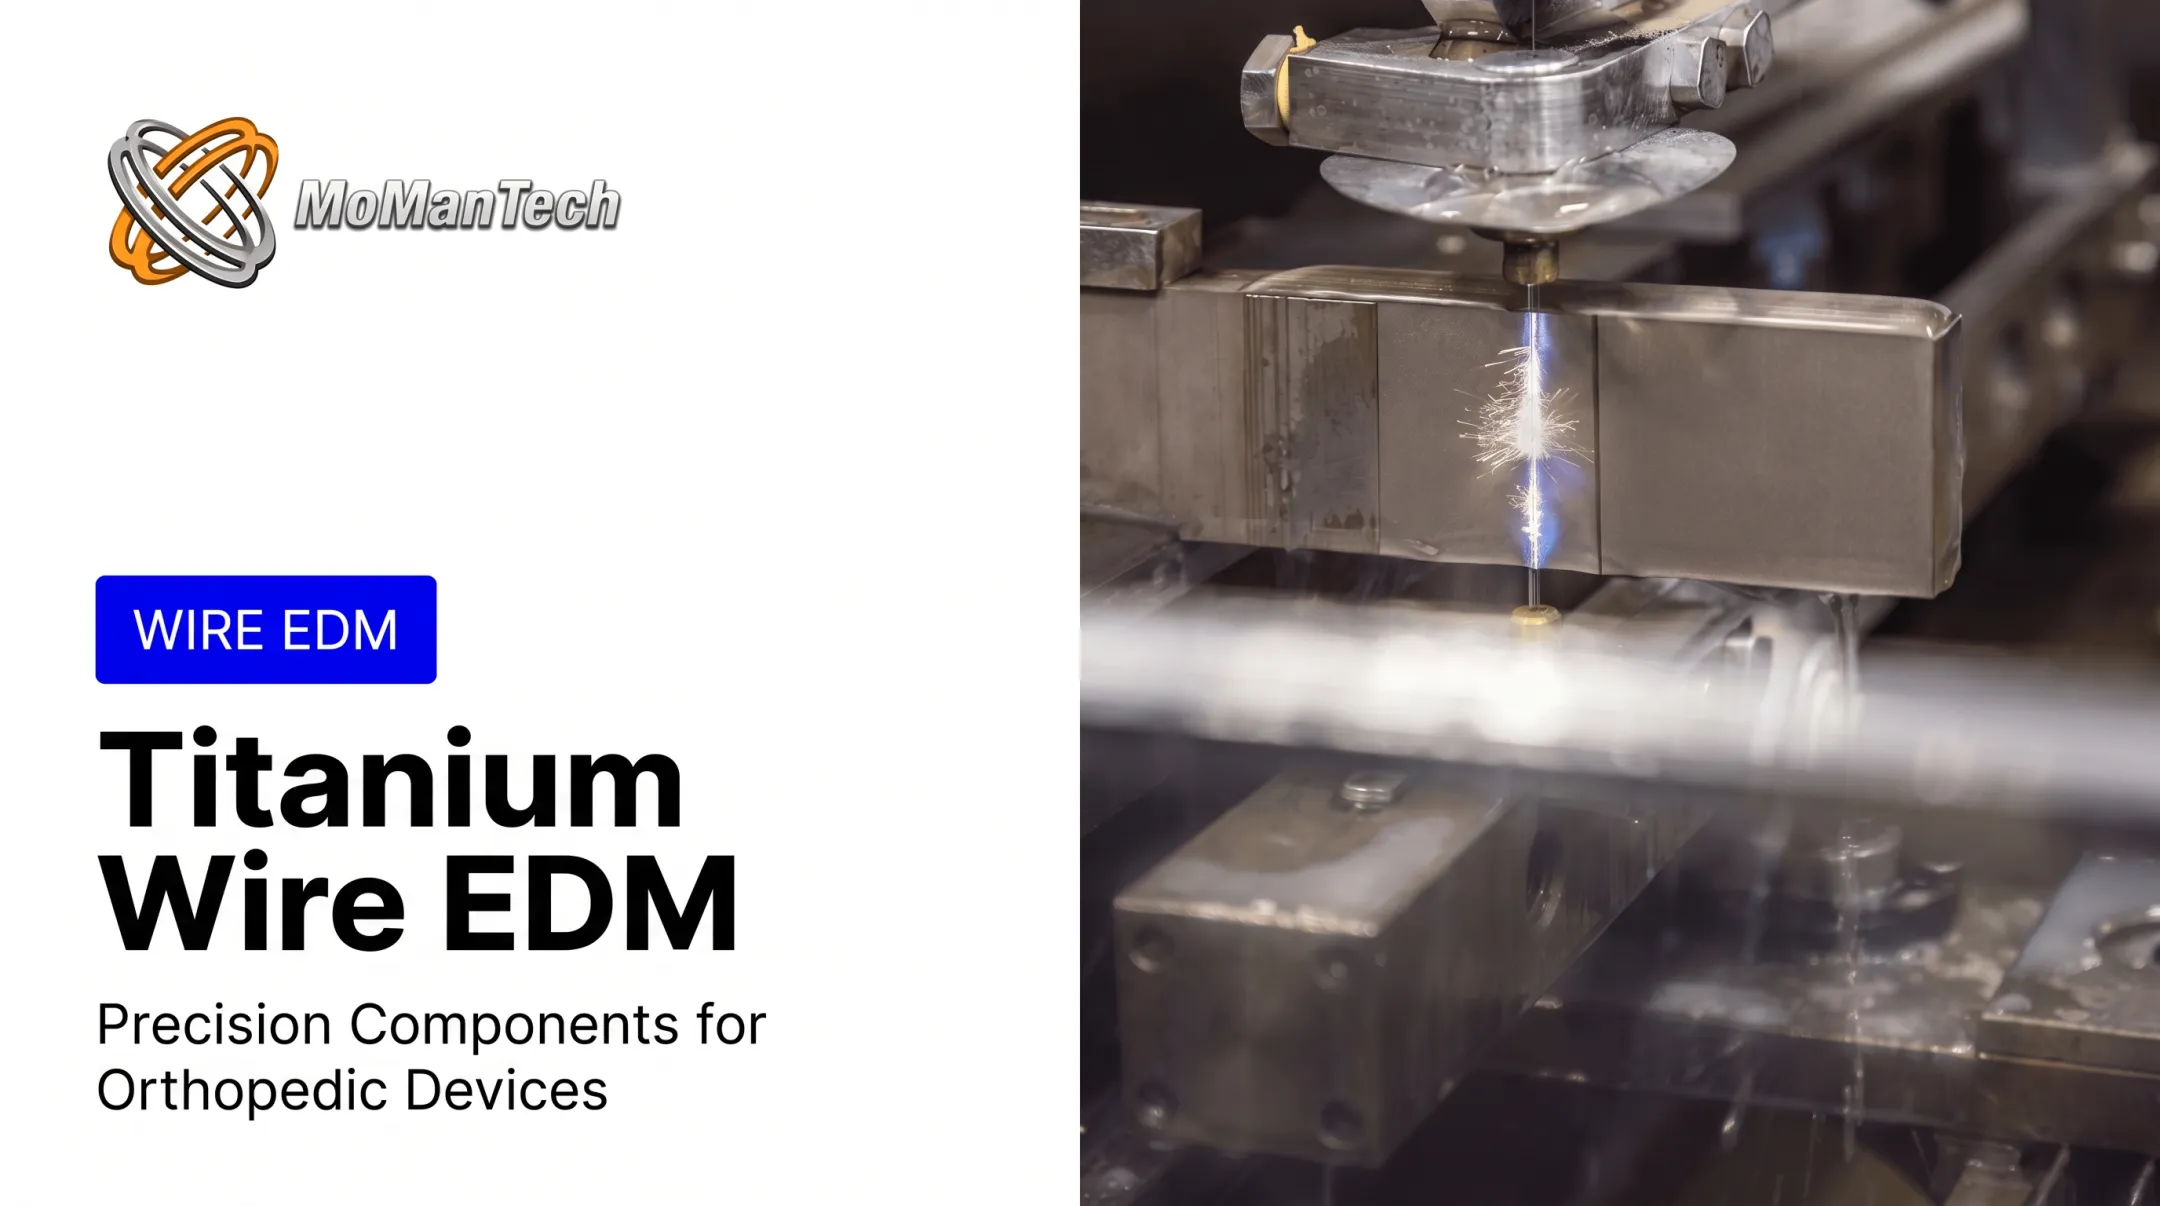
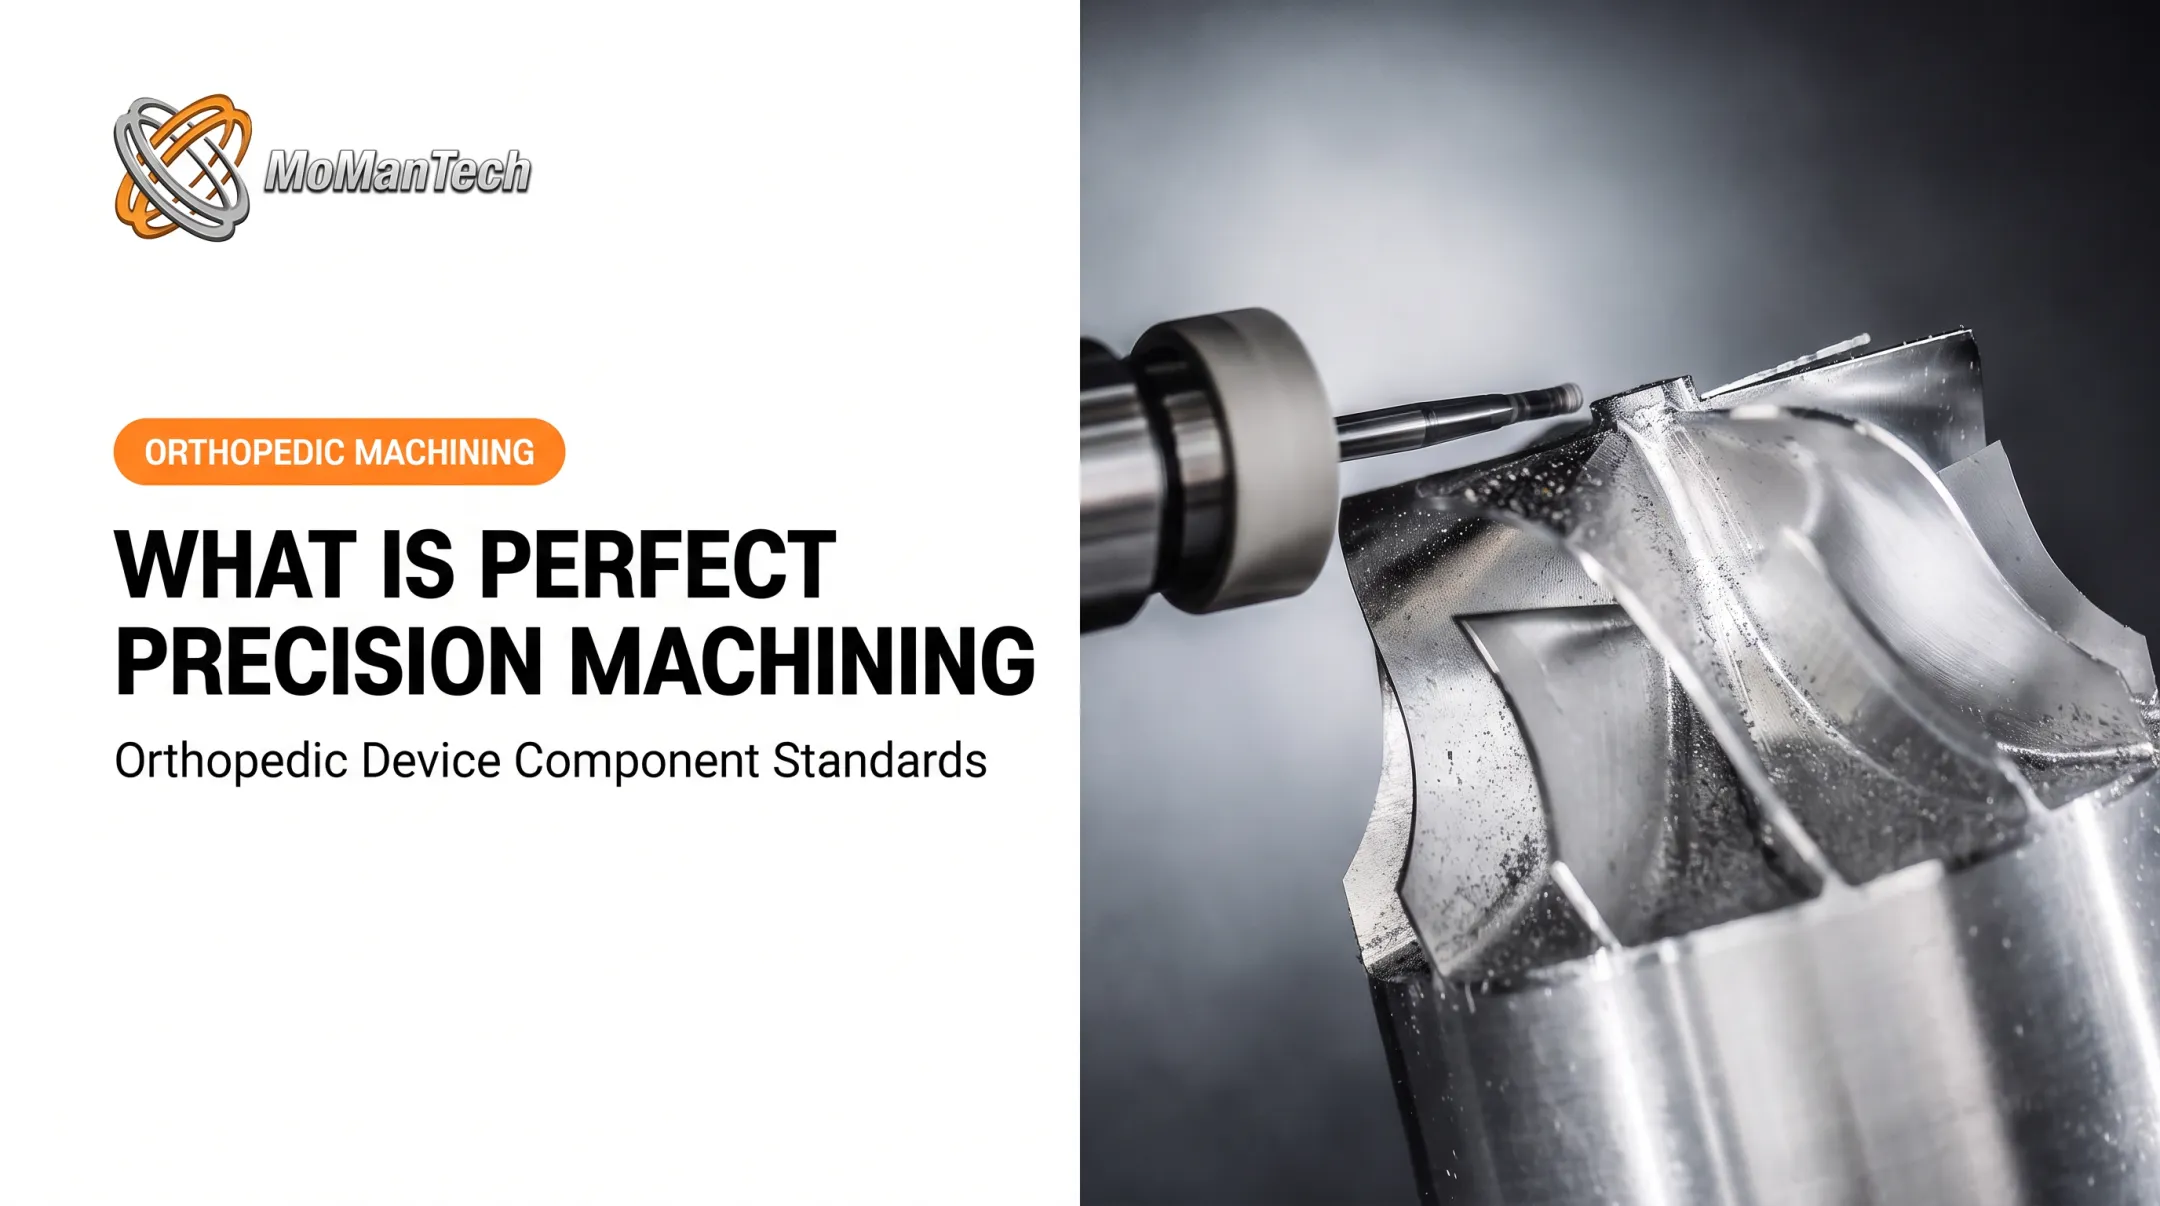
Milled titanium is a titanium workpiece that's been shaped, drilled, or finished using a CNC milling machine. The term describes the finished titanium part, cut to tolerance by a rotating cutter.
Titanium earns its place in demanding industries because it's lightweight, strong, corrosion-resistant, and biocompatible.
According to Kennametal's milling guide, a mill rotates a cutter against the workpiece while the table moves the material around it, removing stock to create the final shape. Applied to titanium, that process demands more than a sharp tool.
Milling titanium well means controlling heat, rigidity, tooling, and chip formation at the same time. This guide covers titanium's properties, common machining challenges, tooling and process decisions, cutting parameters, medical-device applications, and what to look for in a manufacturing partner.
Key Takeaways
- Titanium resists heat dissipation, reacts with cutting tools, flexes under load, and can work-harden if cutting conditions aren't controlled
- Reliable results depend on the full system: alloy, machine, toolholder, cutter geometry, coolant, workholding, programming, and inspection
- Speeds, feeds, and engagement values are starting points to validate against your alloy, tool, and machine
- Medical-device OEMs should evaluate both machining capability and quality-system maturity before choosing a titanium partner
Why Is Titanium Difficult to Mill?
Titanium's reputation for being hard to machine comes down to a handful of physical properties working against you at once.
The Core Material Challenges
Titanium's strength-to-weight ratio is excellent for finished parts, but that same strength resists cutting forces. Combine that with low thermal conductivity, and heat has nowhere to go except into the tool edge. Ti-6Al-4V conducts heat at roughly 6.6 W/m-K, a fraction of what steel manages, according to TIMET's technical data on the alloy.
Titanium also tends to chemically react with cutting tools, causing smearing, galling, and welding at the cutting interface. Its lower elastic modulus means the material deflects away from the tool rather than shearing cleanly, which hurts dimensional accuracy. And if the cutter rubs instead of cutting, that friction work-hardens the surface, making the next pass even tougher.
Failure Modes to Watch
Keep an eye out for these warning signs during a titanium milling operation:
- Excessive heat buildup at the cutting edge
- Built-up edge or chip welding on the tool
- Accelerated flank wear or edge chipping
- Chatter from insufficient rigidity or excessive engagement
- Tool deflection causing dimensional drift
- Poor surface finish from rubbing or vibration
CP Titanium vs. Ti-6Al-4V
Not all titanium behaves the same way under a cutter. Commercially pure (CP) titanium is softer and gummier, which creates adhesion and chip-control problems. Ti-6Al-4V brings higher tensile strength and lower thermal conductivity, increasing both force and heat demands. Treat these as distinct materials with distinct starting conditions, not interchangeable grades.
Geometry matters too. Interrupted cuts, deep cavities, thin walls, and long tool overhangs all increase risk because they add vibration, reduce rigidity, or trap heat.
Diagnosing Problems in the Field
A quick diagnostic sequence helps isolate the cause:
- Chatter usually points to rigidity or excessive radial engagement
- Welded chips typically trace back to heat buildup or poor chip evacuation
- Premature wear often signals wrong cutting data or unsuitable tool geometry
- Dimensional drift frequently results from tool deflection or thermal expansion
How Is Titanium Milled? Machines, Tooling, and Workholding
Getting titanium milling right starts with the machine itself, not just the cutter.
Machine and Fixturing Requirements
A machine built for titanium needs:
- Structural rigidity and stable axis motion
- Spindle torque at low-to-moderate speeds
- Coolant delivery that reaches the cutting zone
Secure workholding and short tool stickout cut deflection and vibration, two of the biggest threats to dimensional accuracy in titanium work.
Tooling Selection
Different operations call for different tools:
- Roughing favors tools designed for high material removal with adequate chip clearance
- Semi-finishing and finishing typically use tighter tolerances on runout and edge prep
- Slots, pockets, and deep cavities often benefit from variable-pitch or variable-helix designs to reduce harmonics
Solid carbide and indexable cutters both have a place, depending on tool diameter, length, and the specific feature being cut. Flute count, edge preparation, and coating selection all shift based on the operation. No single setup works for every job.
Climb vs. Conventional Milling
According to Sandvik Coromant's guide on milling direction, climb (down) milling reduces chip thickness from entry to exit. That path is often preferred when the machine, fixture, and workholding can handle the forces involved.
Conventional (up) milling starts with zero chip thickness, so the tool rubs before it cuts, generating heat and accelerating wear. Climb milling can pull the workpiece into the cutter if backlash isn't controlled, so machine condition matters as much as the theory.
Coolant and Chip Control
Titanium milling needs enough coolant volume and pressure to reach the cutting zone, not just flood the general area. Chip recutting is a real risk, especially in pockets, so chip evacuation strategy deserves as much thought as the toolpath itself. Through-tool or high-pressure coolant delivery can help where the machine supports it.
Roughing Strategy Selection
Adaptive, high-efficiency, trochoidal, plunge, and radial roughing strategies all have their place. The right choice depends on part geometry, available machine capability, tool length, and how much cutting force the setup can tolerate.
A practical validation approach: Review the alloy and geometry first. Choose conservative starting parameters. Run the operation and inspect chip color and shape, along with tool condition. Then adjust one variable at a time, rather than changing speed, feed, and engagement all at once.

Titanium Milling Parameters and Toolpath Optimization
Cutting parameters interact with each other. Change one, and the others shift in response.
The Core Relationships
Spindle speed, surface feet per minute (SFM), chip load (feed per tooth), feed rate, flute count, axial depth of cut, and radial engagement all combine to determine material removal rate. There's no single "correct" SFM for titanium milling.
Starting values depend on the specific alloy, the tool manufacturer's recommendation, coating, and the operation being performed. Always validate published starting ranges against your toolmaker's current data and your own machine before committing to a production run.
Why More Speed Isn't Always Better
It's tempting to assume higher spindle speed means faster cycle times. With titanium, more speed usually means more heat at the cutting edge.
A lower surface speed paired with the right engagement and feed strategy often protects the edge better than an aggressive RPM setting, especially in roughing where heat builds quickly.
Engagement Strategy Tradeoffs
High-efficiency milling (HEM) approaches use low radial engagement with higher axial depth, spreading wear across more of the cutting edge. Alternative engagement strategies trade this off differently:
| Factor | Low radial engagement (HEM) | Higher radial engagement |
|---|---|---|
| Heat generation | Lower, spread across edge | Higher, concentrated |
| Tool life | Often extended | Can shorten |
| Tangential force | Lower | Higher |
| Machine load | Lower | Higher |
| Workholding demand | Moderate | Higher |
Helical's HEM test on Ti-6Al-4V, published in 2020, reported 20% longer tool life using an HEM-style tool compared to a standard six-flute cutter, with a baseline of 400 SFM and 120 IPM.
That's a tool-design comparison within HEM-style cutting, not proof that HEM universally beats conventional milling. Treat it as evidence to validate, not a number to copy directly.

Adjusting for Difficult Features
Thin walls, deep pockets, long tool reach, interrupted cuts, and small-diameter tools all need parameter adjustments. There's no universal percentage reduction that works across the board. Instead:
- Reduce radial engagement where deflection risk is high
- Slow feed rates in interrupted cuts to reduce shock loading
- Shorten tool stickout wherever the geometry allows
- Use lighter finishing passes to protect surface integrity
A compact starting checklist:
- Confirm alloy and condition (for example, Ti-6Al-4V annealed vs. ELI)
- Pull current speeds/feeds from the toolmaker, not a generic chart
- Calculate RPM: (SFM × 3.82) ÷ tool diameter (inches)
- Calculate feed rate: RPM × number of flutes × chip load per tooth
- Verify against machine torque curve and workholding capacity
- Run a conservative first pass, inspect, then adjust incrementally
Titanium Applications and Medical-Device Manufacturing
Titanium shows up across a wide range of industries:
- Aerospace: jet-engine components and airframe structures
- Chemical processing: corrosion resistance in harsh environments
- Marine and energy: seawater and brine exposure
- Dental: well-established implant use cases
For MoManTech, the orthopedic space is where titanium milling matters most.
Why Titanium Works for Orthopedic Devices
The International Titanium Association ties titanium's biocompatibility to its corrosion resistance, strength, and relatively low modulus. Those same properties support osseointegration, the bonding between implant and bone. Add titanium's favorable strength-to-weight profile, and it is clear why the metal shows up so often in orthopedic implants and instruments.
Two ASTM standards govern implant-grade material: F67 covers unalloyed (CP) titanium for surgical implants, while F136 covers wrought, annealed Ti-6Al-4V ELI. These specify material requirements, not machining practices.
A machined part can meet dimensional print requirements and still need separate verification for biocompatibility, sterilization suitability, and regulatory clearance. Machining capability and material certification are related but distinct conversations.
Representative Machined Components
Orthopedic OEMs typically need titanium parts across several categories:
- Spinal implant components and related surgical instruments
- Trauma and large-bone fixation components
- Foot-and-ankle or extremity device parts
- Complex surgical instrumentation supporting implant placement
MoManTech works with orthopedic medical-device OEMs across these categories, supporting prototype quantities as small as 1-10 units through production runs of 100 or more. That range matters for startups that need a first article before committing to volume, and for established OEMs placing repeat production orders.
Design-for-manufacturability input happens early, before a print gets locked in, which tends to reduce rework later in the program.
Quality, Inspection, and Choosing a Titanium Machining Partner
Milling the part correctly is only half the job. Proving it was made correctly is the other half, especially in orthopedic manufacturing.
Quality Controls That Matter
Look for these elements in any titanium machining process:
- Material certification tied to the specific alloy and condition ordered
- Revision control so the latest print is always the one in production
- In-process and final dimensional inspection, not just a one-time check
- Surface-finish verification and burr control
- Lot traceability from raw material to finished part
- Documented nonconformance handling when something doesn't meet spec
Questions Worth Asking a Potential Partner
Medical-device OEMs should ask about:
- Quality-system certification
- First-article inspection procedures
- Process validation where applicable
- Inspection equipment capability
- How long records get retained
Requirements shift over time, so verify current expectations through authoritative regulatory sources rather than older guidance.
A Supplier Evaluation Checklist
Before committing to a titanium machining partner, confirm:
- Direct experience with your specific alloy and part geometry
- Support for both prototype and low-volume production
- Scalability to production quantities without re-qualifying the process
- Engineering responsiveness during design iteration
- Automation that supports consistent quality at higher volumes
- Clear communication and realistic lead-time expectations
MoManTech is ISO 13485:2016-certified and works exclusively within orthopedic medical-device manufacturing, covering spine, trauma, large joint, and foot/ankle components. The shop's inspection setup includes CMM and laser measurement capability alongside standard gaging, and every component gets inspected before it leaves the facility.

Automated loading and unloading support higher-volume runs without pulling skilled machinists off other work. That capacity helps with responsiveness when a customer needs a fast turn on a first article.
If you're evaluating a titanium machining partner for an upcoming implant or instrument program, talk through your specific alloy, geometry, and volume needs before locking in a supplier.
Frequently Asked Questions
What products are made out of titanium?
Titanium shows up in aerospace structures and jet engines, medical and dental implants, chemical-processing equipment, marine components, and energy-industry piping. Its corrosion resistance and strength-to-weight ratio make it valuable across all these sectors.
What is the recommended SFM for milling titanium?
There's no single universal SFM value. The right starting point depends on the alloy, cutter design, coating, machine capability, and radial engagement. Check current data from your tool manufacturer and validate it on your own setup before running production.
How is titanium machined?
Titanium is typically machined through CNC milling or turning, using rigid setups, suitable carbide tooling, and controlled coolant delivery to manage heat. Conservative, validated cutting data combined with careful chip evacuation and thorough inspection round out a reliable process.
Why is titanium difficult to mill?
Titanium retains heat due to low thermal conductivity, reacts chemically with cutting tools, deflects under force because of its elasticity, and can work-harden if rubbed rather than cut cleanly. These combined factors accelerate tool wear and increase the risk of chatter.
How do you choose a titanium milling partner for medical-device components?
Look for direct experience with your titanium alloy and part type, ISO 13485:2016 certification, and support across prototype-to-production volumes. Design-for-manufacturability input, documented inspection practices, and responsive communication all matter just as much as machine capability.